

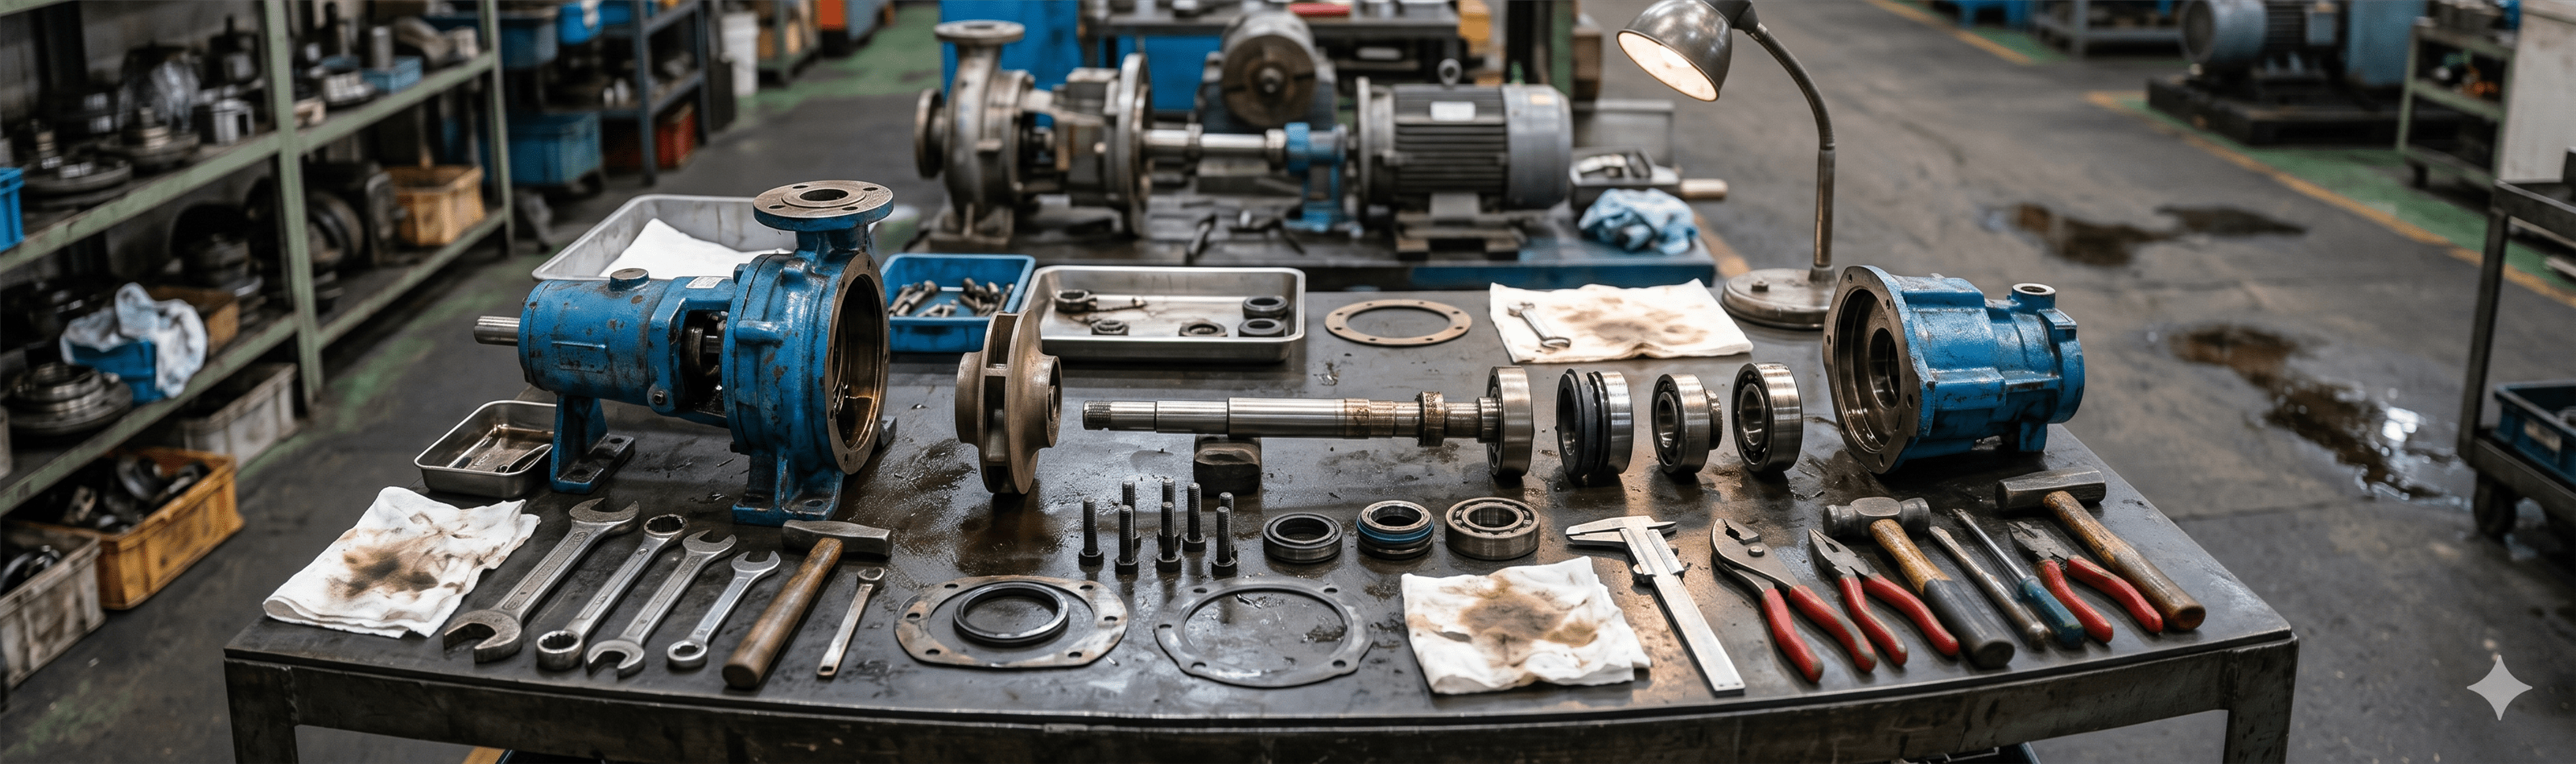
When introducing vibration monitoring for anomaly detection in rotating machinery such as pumps within a factory, the first difficulty the field faces is "threshold setting." On this page, based on a case study of anomaly detection in a centrifugal pump at a major automobile manufacturer's plant in Mie Prefecture, we explain the limitations of absolute value indicators and the know-how of "trend management" that is truly useful in the field.
In vibration evaluation, absolute value indicators shown by ISO and others are merely guidelines.
In actual maintenance fields, normal vibration values vary greatly from one machine to another depending on the installation environment and operational conditions.
Even if normal evaluation is difficult, vibration values will show a clear change (upward trend) if a mechanical anomaly progresses. Therefore, rather than adhering to absolute value judgments, it is extremely important to perform trend management based on the "usual state" of each equipment. Rather than spot diagnosis by high-performance analyzers, comprehensive and high-frequency data collection using inexpensive sensors is the key to predictive maintenance.
When practicing trend management, care must also be taken in selecting the measurement direction.
Trend management using the "3-axis composite value" calculated by the Pythagorean theorem is convenient and simple, but it is essential to understand the vibration characteristics in each direction at the initial stage of introduction. This is because tracking fluctuations in a specific direction (such as the radial direction of the rotating shaft) is often more effective for anomaly detection.
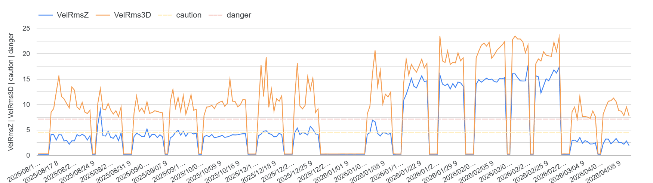
*Figure: Comparison graph of the 3-axis composite vibration value and the Z-axis (radial direction of the rotating shaft) during anomaly detection of a centrifugal pump.
Even in the centrifugal pump anomaly detection case introduced this time, it has been confirmed as actual data that the fluctuation range is larger in the Z-axis direction compared to the 3-axis composite value, allowing signs of anomalies to be judged earlier and more clearly.
Even with similar equipment, accumulating individual quirks and characteristics as data and reading those changes is the very core of maintenance know-how in the field. The wireless vibration meter "conanair" utilizes the patented under-sampling technology to accumulate raw data from the field in a lightweight and high-frequency manner. It supports a shift to reliable, data-driven predictive maintenance by building an environment where maintenance personnel can easily perform "trend management" themselves.
| Company Name | NSXe Co.Ltd - Nakayama Hydrothermal Industry Co., Ltd. |
|---|---|
| Head Office | 7686-10 Hirano-cho, Suzuka, Mie513-0835, Japan zip code 513-0835 |
| Phone | +81-90-2189-1398 |
| FAX | +81-59-379-4704 |
| Business Hours | 8:00~17:00 |
| Office Regular Holiday |
Saturday afternoons, Sundays and public holidays |
| URL | https://conanair.com/ |
| Company Name | NSXe Co.Ltd - Nakayama Hydrothermal Industry Co., Ltd. |
|---|---|
| Head Office | 7686-10 Hirano-cho, Suzuka, Mie513-0835, Japan zip code 513-0835 |
| TEL | +81-90-2189-1398 |
| FAX | +81-59-379-4704 |
| Business Hours | 8:00~17:00 |
| Office Regular Holiday |
Saturday afternoons, Sundays and public holidays |
| URL | https://conanair.com/ |